
Rebecca Schaevitz,
CPO and Co-founder
What Inference is Changing at the Box Edge
Radix has become central to the scale-up conversation. The connector is the central point where radix becomes a piece of hardware. The industry has a good figure of merit for the optical engine. The connector has no such consensus with every vendor defining the metric differently.
Rebecca Schaevitz, Chief Product Officer and co-founder of Mixx Technologies, says the connector needs one of its own.
“Terabits per millimeter is dependent on the number of wavelengths per fiber, and whether it’s single direction or bidirectional, so you’re starting to conflate the engine technology with pure radix,” she says. “The connector is what’s supporting the pure radix, and that’s really based on the number of fibers.”
“I think it’s fibers per millimeter squared,” she says. “Density at the box edge is effectively the right metric.”
One problem, not four
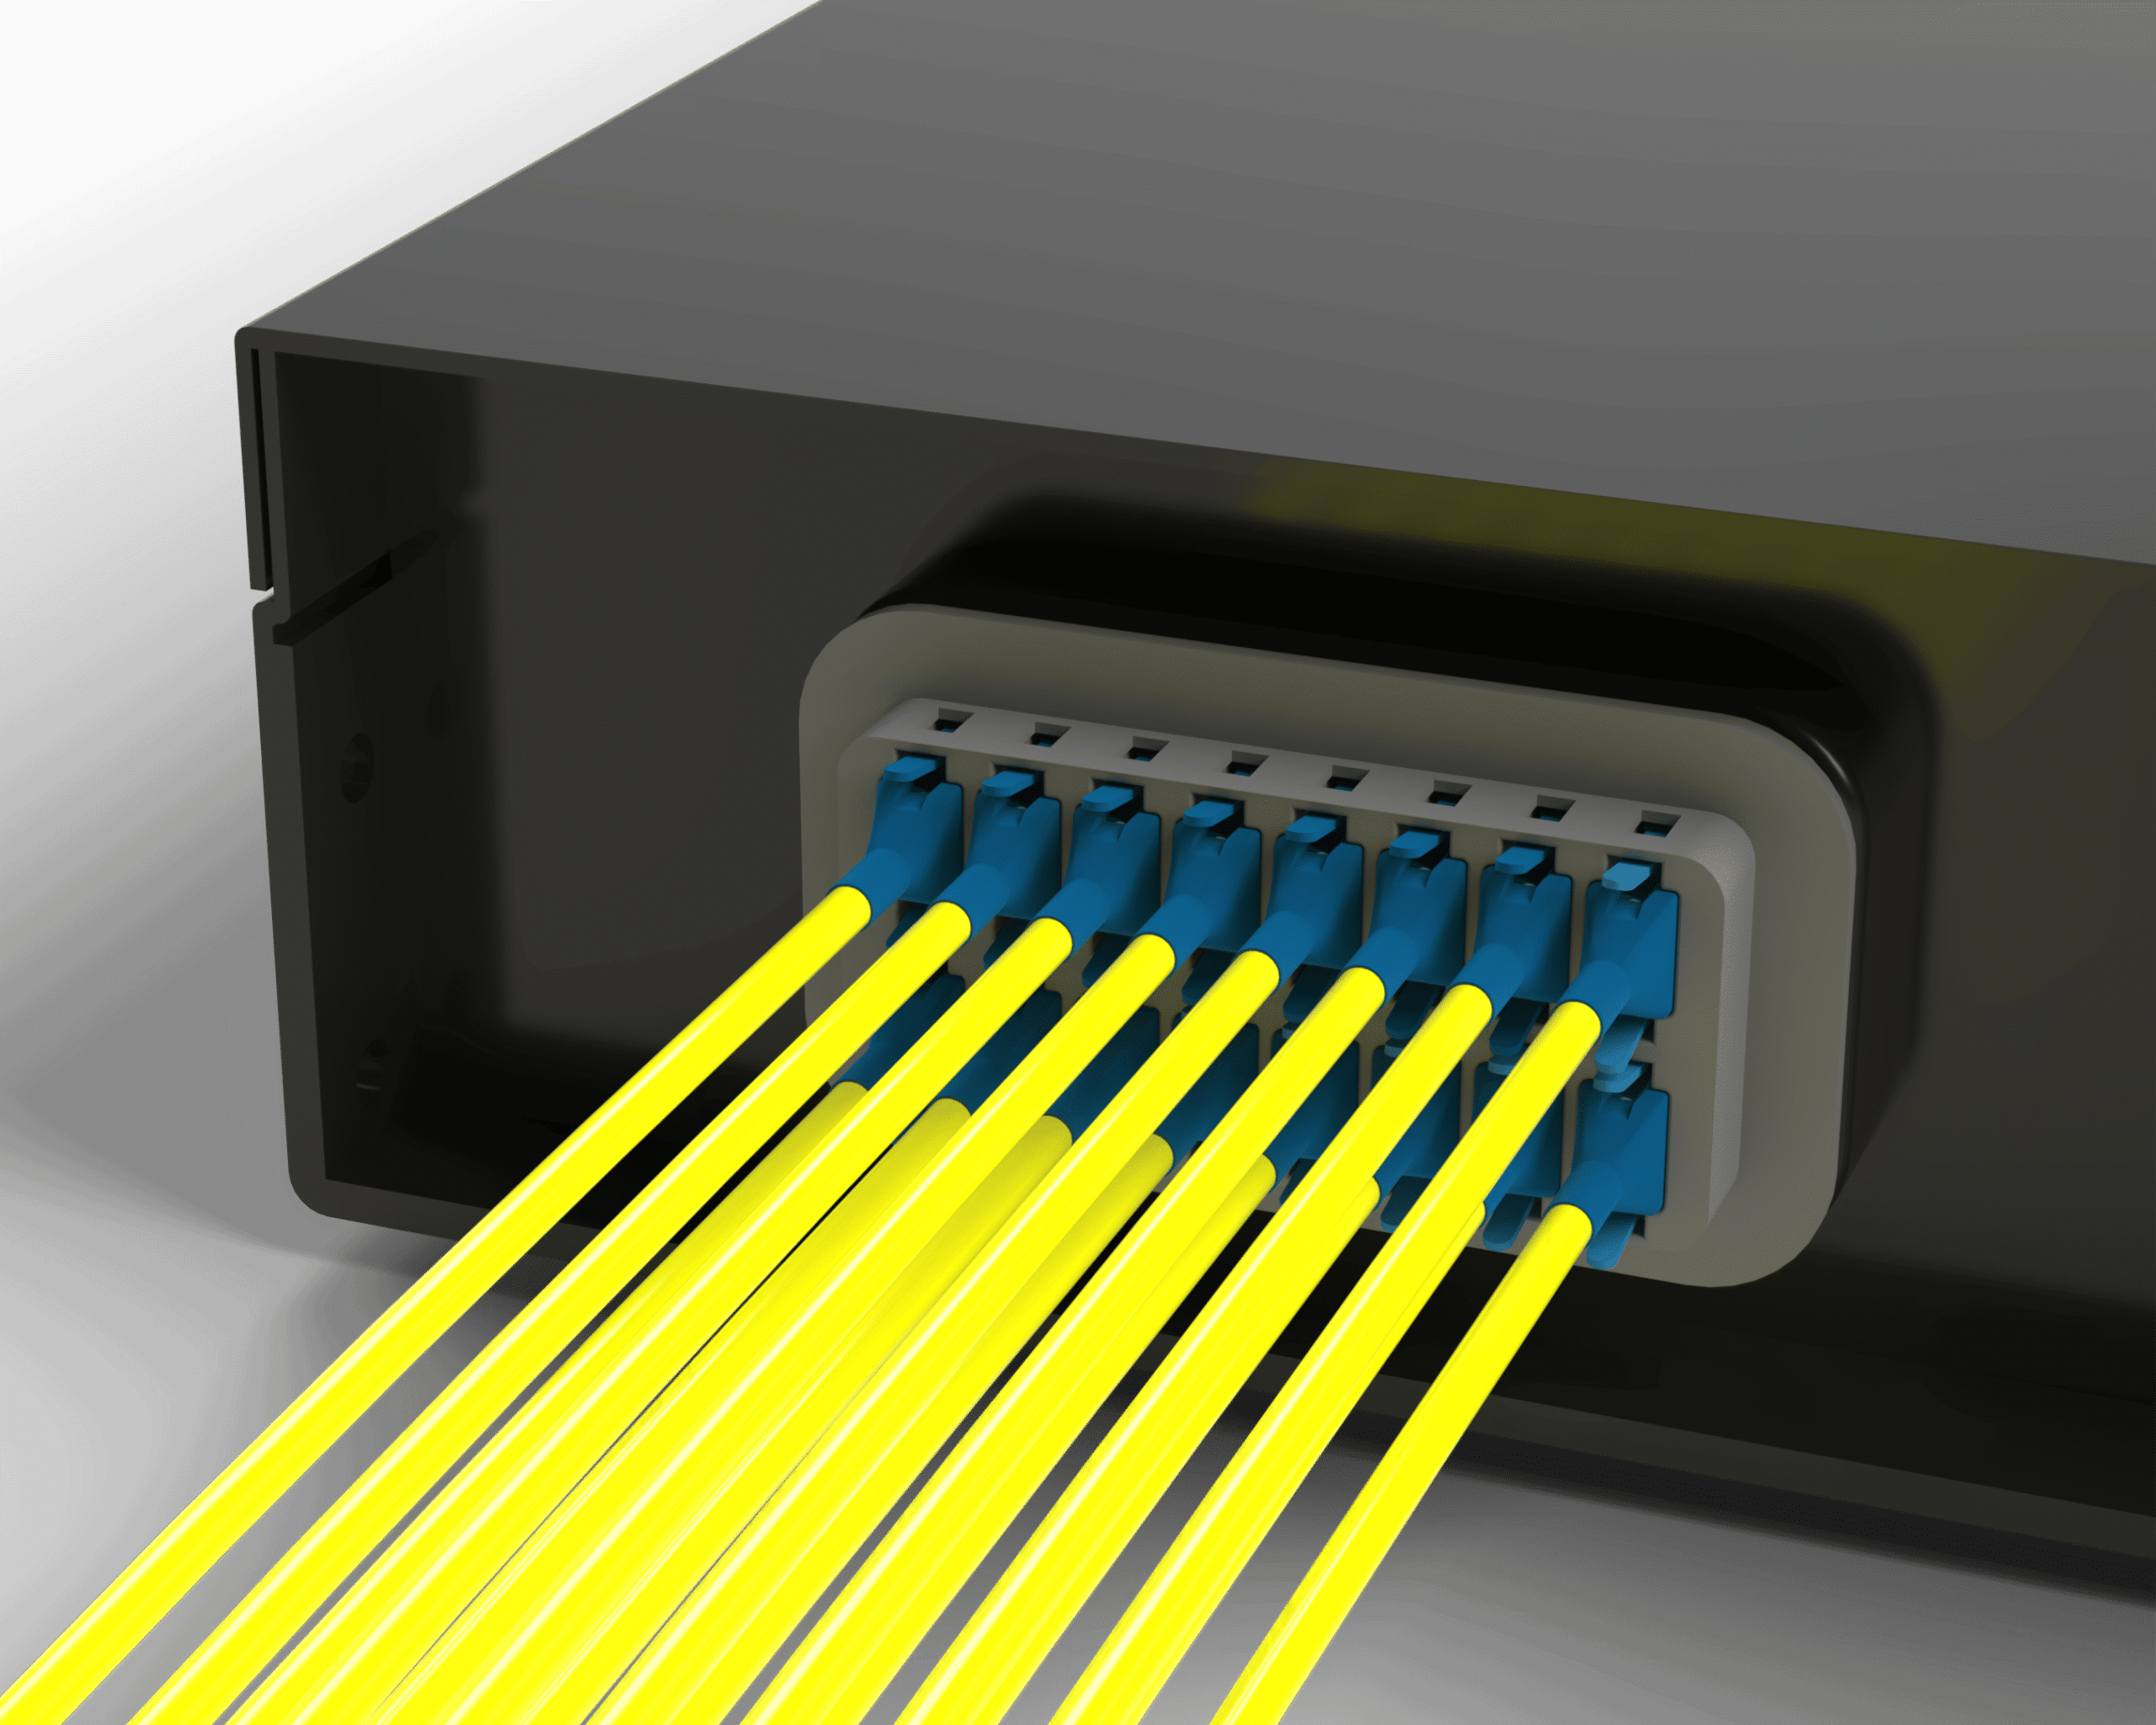
The industry has built the connector as four separate problems: one part for the package, one for the laser, one for the front panel, one for the backplane. Launching this week, Mixx has built one ferrule technology that terminates all four: The SxCTM Connector.
Schaevitz frames Mixx’s approach as a volume argument.
“The basic fundamental promise of scale is doing the same thing many times and optimizing it,” she says. “We treated this as one problem that had to be solved cohesively across the system.”
Schaevitz puts the payoff in qualification terms. “It allows you to more easily get to the volumes that are needed,” she says. “You can qualify it in terms of reliability, because you’re using standard processes that are automated.”
“Bringing in automation brings in consistent process flow, which brings in quality and reliability of the product,” she says. “It’s very different from the historical artisan approach that optics has taken.”
The ferrule itself is glass, and it is not made one part at a time. “It’s a wafer-scale process, done in the same way that silicon is done today,” she says.
Where it goes to work?
The SxCTM Connector goes to work in three places, and each asks something different of the same part.
The front panel is the human side: connectors seat and unseat by hand, and often. “You’re doing a hand change of that connector assembly more frequently, so you just need a little bit more room to facilitate that,” Schaevitz says. What it gives up in spacing it recovers in consistency, and she attributes that to the process rather than the part: running the manufacturing flow at wafer scale holds performance steadier than butt-coupled fiber technology can.
The backplane inverts the problem. Fiber comes out the back of the box instead of the front, the electrical backplane becomes optical, and connection moves to the bulkhead level, whole fields of fibers mating at once. The individual connector is handled once or twice during manufacturing validation, then buried. “You can’t simply take a jumper and replace the jumper,” she says. Anything that goes wrong in there has to have been designed out before the box went in.
Behind both sits the shuffle box, where fibers from one connector fan out to dozens more and yield compounds connector by connector. “Because our process enables consistency in performance, we can enable more complex shuffle schemes,” she says.
One technology meets three insertions, density, and handling requirements without becoming three parts.
What the connector of the future has to do?
Schaevitz names four things any connector has to do to carry this era.
Density comes first, counted in fibers rather than bandwidth.
Power handling follows. “You’re seeing laser sources that are starting to disaggregate in the network and be placed elsewhere,” she says, and multi-wavelength signals add load at the I/O itself. Plastic is incapable of carrying it. “Plastic, because it’s an organic material, has inclusions and organic particles,” she says. “You cannot easily control where that material lies in the optical path.” Fused silica carries no such contaminants.
Then there is dust. Backplane connectors sit exposed in the rack before a server box goes in. Any particle that lands during that window can take a link down. Cleaning it once is not the requirement. Not having to clean it again is. “We need to have timelines where we’re going five years in use and dust is not an issue,” Schaevitz says, “where they don’t have to go and re-clean it because particles start accumulating over time and cause failures in their network or system.” Non-contact geometry is what changes the failure mode. “If there’s a failure immediately because a large piece of dust somehow got on there, you can simply blow it off and it’s fixed,” she says. “In traditional connectors, if that large dust is there, it has caused a scratch on the surface during the insertion process, and you have a complete failure at that point.”
Volume manufacturability is the one she believes the industry underestimates. “The ferrule supply itself maybe is not the limitation,” she says. “It is more likely the cable assembly.” The assembly work that follows the ferrule is still largely handwork. “All of that goes into diminished capacity to produce, especially if you’re doing rework,” she says. The scaling question is bigger than sourcing. “That’s the full supply chain, but also how things are put together: how many units per hour can you get out, versus however many hours per unit?” she says.
Why the connector?
Schaevitz holds a doctorate in silicon photonics and spent time at Corning, where she saw what scaling fiber manufacturing costs, and at Broadcom, where she worked on connectors for co-packaged optics. She co-founded Mixx to solve a problem she saw from both sides.
Schaevitz splits the proving into two stages. Time zero is the part as manufactured: “insertion loss, durability testing, making sure you can insert and reinsert multiple times and get the same performance metrics out of it, and measuring the back reflection.” She calls that half relatively simplistic. What is not simplistic is doing it across volume production and lifetime. “In our case, that would be each wafer that’s manufactured, verifying that we still get consistency from wafer to wafer,” she says. Lifetime is what survives temperature cycling, humidity at high temperature, shock and vibration. “The quantities will also have to increase in order to demonstrate that reliability over lifetime for the magnitude of parts the industry requires.”